跳至主要内容

SELECTION PRINCIPLE OF CUTTING PARAMETERS FOR SCREW THREAD TURNING

Because the pitch (or lead) of the thread is specified by the drawing, the key to choose the cutting parameters when turning the screw thread is to determine the spindle speed n and the cutting depth AP.

1) SELECTION OF SPINDLE SPEED TO DO SCREW THREAD TURNING

According to the mechanism that the spindle turns 1 and the cutter feeds 1 lead when turning the thread, the feed speed of the CNC lathe is determined by the selected spindle speed. The thread lead (which is the pitch when the thread is single head thread) instructed in the thread processing program section is equivalent to the feed speed VF VF = n f (1) expressed by the feed rate f (mm / R)
From Formula 1, it can be seen that the feed speed VF is proportional to the feed amount F. if the spindle speed of the machine tool is selected too high, the converted feed speed will greatly exceed the rated feed speed of the machine tool. Therefore, when selecting the rotation speed of the main shaft for turning the thread, the parameter setting of the feeding system and the electrical configuration of the machine tool should be considered to avoid the phenomenon of “disordered thread” or the thread pitch near the start / end point not meeting the requirements.
In addition, it is worth noting that once the thread processing is started, the spindle speed value cannot be changed generally, and the spindle speed including finishing must follow the selected value during the first feed machining. Otherwise, the CNCsystem will lead to “disordered thread” due to the “overshoot” of the reference pulse signal of the pulse encoder.
Aluminum Precision Machining Part

2) SELECTION OF CUTTING DEPTH TO DO SCREW THREAD TURNING

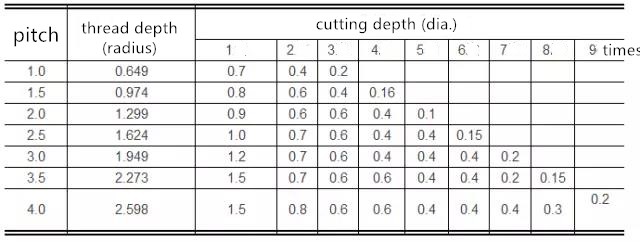
Because the thread turning is a forming turning, the strength of the cutting tool is poor, and the cutting feed is large, and the cutting force on the cutting tool is also large. Therefore, it is generally required to select a relatively reasonable cutting depth according to the decreasing trend. Table 1 lists the feed times and cutting depth reference values of common metric thread cutting for readers to consult.
Table 1 feed times and cutting depth of common metric thread cutting
feed times and cutting depth of common metric thread cutting

KYLT Precision CNC machining services (milling & turning service), Fast prototyping, Fixture/Jig/Tooling making,Aluminum die casting & plastic injection parts. Email:cnkylt@aliyun.com +008615195010186
KYLT CNC Machining Services:
KYLT CNC Precision Machined Parts:
More information about Machining Technology:

评论

此博客中的热门博文

SIMPLIFIED DRAWING METHOD FOR MECHANICAL DRAWING

When design  machine parts  /  prototypes  by 2D engineering method, we can adopt simplified drawing method: 1.When the object ( mechanical part ) has several identical structures (teeth, slots, etc.) and distributes according to certain rules, only a few complete structures need to be drawn. The rest are connected by fine lines, and the total number of structures is indicated. Mechanical part  Examples of Simplified Drawing of Mechanical Drawings : Examples of Simplified Drawing of Mechanical Drawings for Same Structure and Simplified Drawing Same Structure and Simplified Drawing 2.A number of holes with the same diameter and regular distribution (round holes, screw holes, sinks, etc.) can be drawn only one or several, the rest can only be represented by the center line, and the total number of holes should be indicated when the size of holes is marked in the figure. Simplified Drawing Method for Regularly Distributed Holes Simplified Drawing ...

WHY SCREW THREAD CAN NOT PASS THREAD GAUGE INSPECTION

After the first metal part be tapped, we always to check it: if pass the thread gauge inspection? The inspection result is OK, we can do mass production. If it fails, We should consider which reasons cause tapping faiulre. KYLT provide Metal Machining services for:  WEDM, EDM, DRILL, TAPPING ,  CNC LATHING ,  CNC MILLING ,  ALUMINUM / MAGNESIUM / PLASTIC RAPID PROTOTYPES MAKING . 1PCS ORDER IS ALLOWED. Aluminum CNC machined workpiece Normally, the following reasons may cause screw thread faiulre: 1) UNQUALIFIED TAP Tap is wear or bad 2) QUALIFIED DRILLING HOLE (BEFORE TAPPING) If the hole is too small, because of friction, will increase the difficulty of tapping, while tapping faster wear, and vice versa, the hole is too big, it can easily tap into, but the quality of teeth is very poor, because the diameter of teeth will become larger, relative to the screw nut bonding force is insufficient, easy to slide teeth. In M3 *0.5, the correct hole (general i...

CNC MILLING: DOWN MILLING &UP MILLING

CNC milling  process adopt  Down milling  or  Up milling ? Which milling method is better? Down Milling & Up Milling Definition Down milling:  refers to the cutting speed direction of the cutter is the same as the moving direction of the workpiece. Up milling : refers to the direction of cutting speed opposite to the direction of movement of the workpiece. CNC milling work, How to distinguish Down Milling and Up Milling. WHEN MILLING WORKPIECE OUTLINE: Clockwise feeding and programming along the outline of the workpiece is Down milling. Counterclockwise programming and feeding along the outline of the workpiece is Up milling. WHEN MILLING THE INNER CONTOUR OF THE WORKPIECE: Clockwise feeding and programming along the inner contour of the workpiece is downmilling. Counterclockwise programming and feeding along the inner contour of the workpiece is reverse milling. CNC UP & DOWN MILLING CHARACTERISTICS OF DOWN MILLING AND UP MILLI...