Spine/Grid Pressure Die Casting Machine – PDC Spine making machine for lead acid battery positive plate.
Lead acid battery positive spine also called positive grid, it is made from lead alloy (PB alloy).
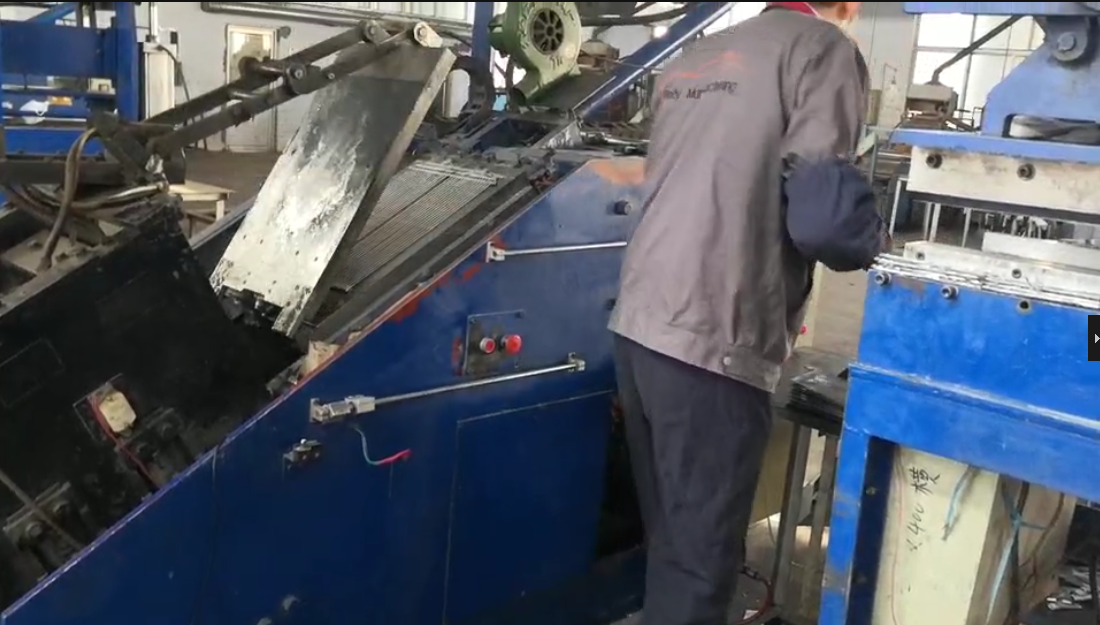
Gravity casting be used to produce the spines many years ago. As its bad performance at the strength and crystal density, pressure die casting method used to instead of old casting method.In Europe, Pressure die casting method are widely used in lead acid battery positive grid manufacturing. The machine be named grid die casting machine, spine die casting machine or pressure spine die casting machine (PDC). Pressure die cast grids (spines) have more advantages than gravity cast spines at the strength and crystal density.
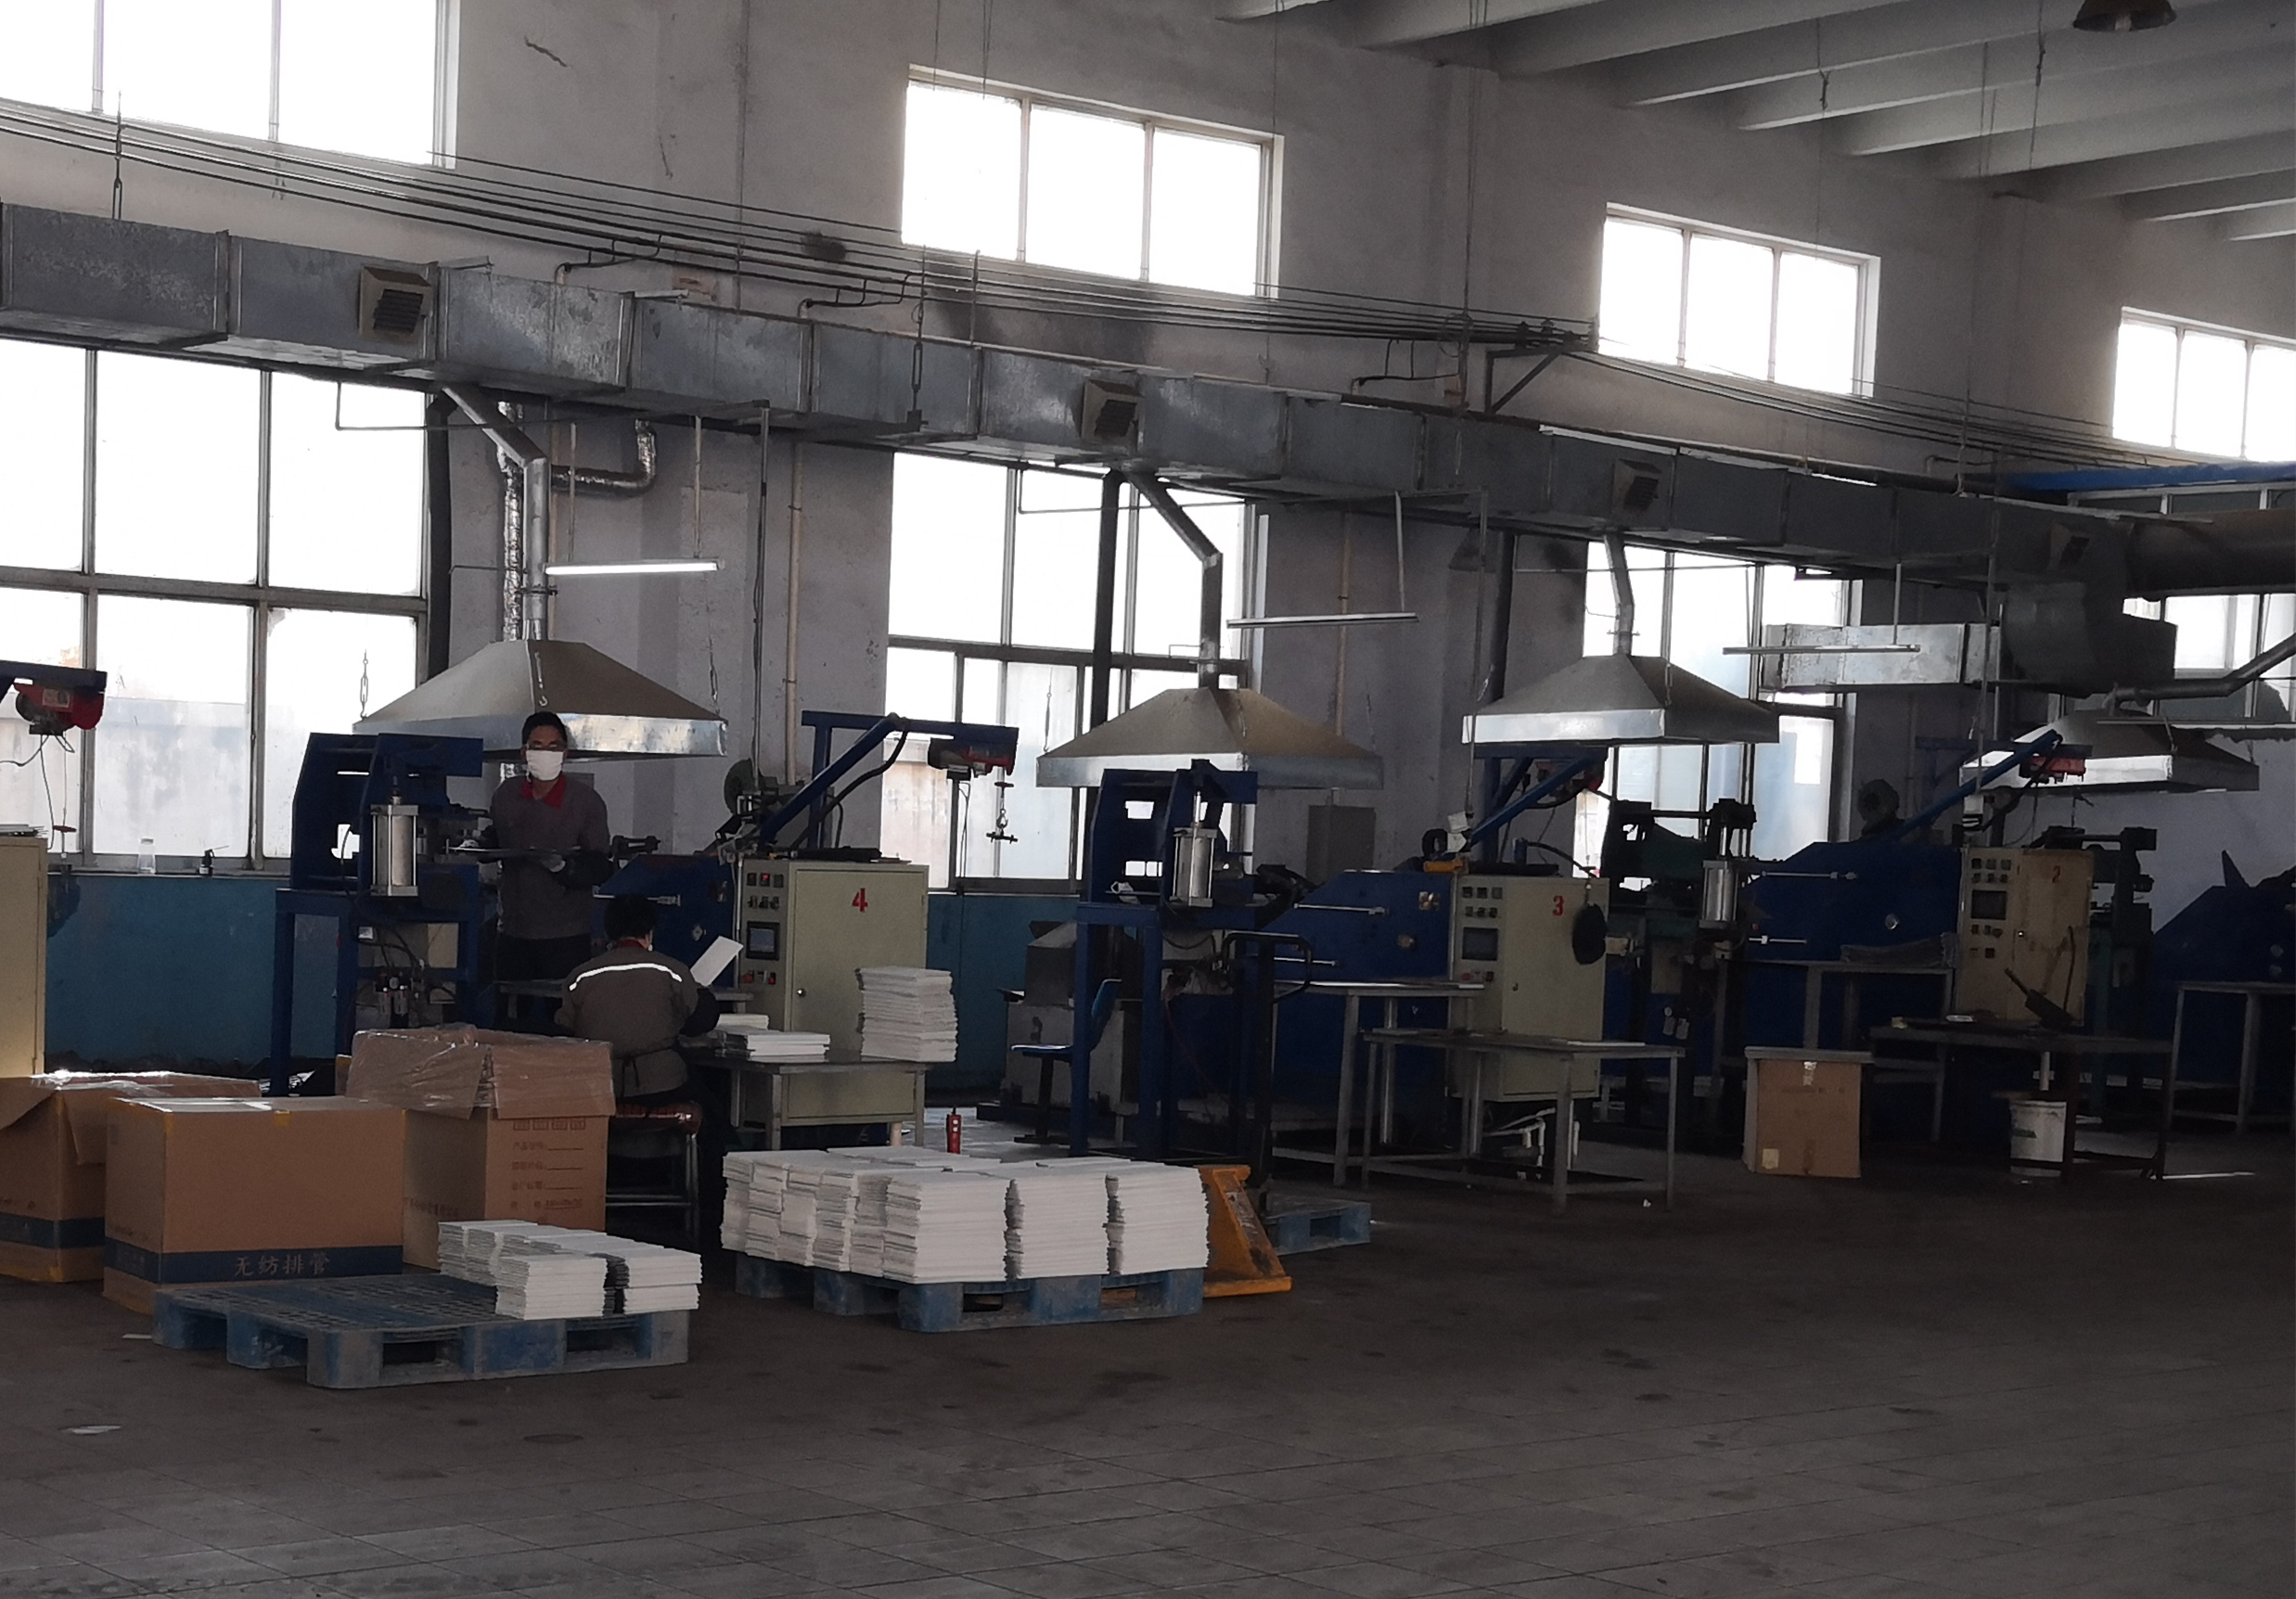
Our die casting machine advantages: stable, easy to maintain. The 700type grid high pressure casting machine with hydraulic mold clamping system, that can make double-spines at one shot.
Basic information of Battery spine/grid die casting machine:
PDC Spine making machine application: to cast tubular positive plates of lead acid battery.
Die casing lead alloy types: Lead antimony alloy, Lead calcium alloy.
Spine PDC machine & Mold working period: Grid Mold 20days, Spine Die Casting Machine 30-40days
Grid Mold material: H13
Mold life: if everything goes well, 3-5years
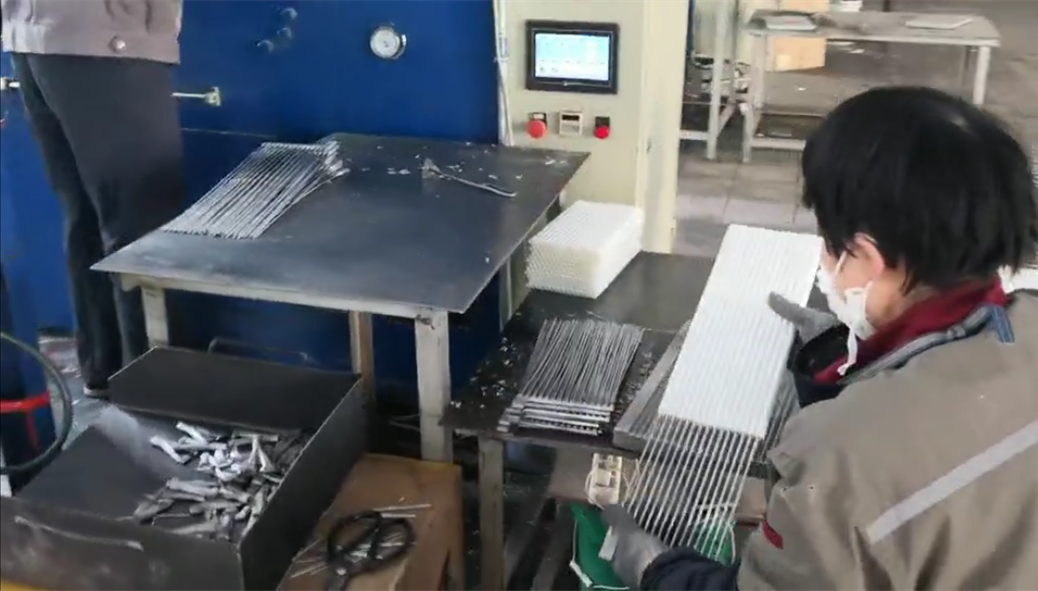
Spine/Grid Pressure Die Casting Machine Performance & Features:
1. PDC grid making machine has 3 kinds control functions: manual, semi-auto, full-auto.
2. Die casting system drives by hydraulic station, pressure and injection speed can be adjusted.
3. Machine Hydraulic system is separated with die casting structure body. An independent hydraulic station gives more space of grid machine for assembly, maintain and repair.

4. Special designed Lifting device used to hoist grid mould (die) conveniently. One person can easily install the mold.

5. Lead(PB) alloy melting pot, injection nozzle and spine mold are heated by electricity. Their temperatures are digitally displayed, all with overheating alarm function.

6. Spine mould heats by electricity and cools by circulating cooling water. Mould temperature can be controlled and adjusted.
7. Mold steel material is H13, which has high strength and hardness.

8. The grids casting process of mold clamping, metal injection, die opening and spine ejection is automatically.
9. Mechanical & Hydraulic clamping methods be used in mold locking process.

10. Machine with PLC & Touch screen, working parameters can be set and control as per program. Monitor shows the actual working data. Operator can read those information conveniently and clearly.

11. Grid cast machine with high efficiency, 2-3 mode /min.
12. Safe and reliable, PLC+ touch screen + grating ruler to ensure safety.
Spine/Grid Pressure Die Casting Machine types:
Spine/Grid Pressure Die Casting Machine specifications:
Spine length (mm) | Spine dia.(mm) | Pot capacity (kg) | Power(KW) | |
PDC-T500 | 2v 15tube Single: L≤430mm; Double: L≤470mm | ≥3mm | 1800 kg | 45KW |
12v EV Single: L≤300mm; Double: L≤210mm | ≥2mm | |||
PDC-T700 | ≤630mm | Spine L 500mm≥3.0mm, 630mm≥3.4mm; EV≥2.0mm | 1800 kg | 45KW |
Service of Spine die casting machine and Spine mold:
1. Choose suitable machine type and making mold as per customer grid drawings.
2. Provide solution, help client to solve problems encountered in production. As per customer demand to improve machine and mold design.
3. Machine and mold, from steel cutting, welding, assembly etc, all processes finished in house.
4. Test machine and mold in house, any problems can solve in factory directly and immediately. Machine and mold test videos are allowed.
5. Free grids samples to buyer for checking.
6. Provide machine & mold operation manual and videos.
7. Provide machine & mold disassembly and packing videos.
8. All disassembly structure parts be marked, easy for assembly in your local factory.
9. Machine be set on a flat cement ground is enough, ready air pressure, cooling water and power. Don't need make special treatment for cement ground.
10. Provide service by videos and online operation guide by computer. (the engineer can indicate
your engineer to operate machine in English.)

More information and price of Spine/Grid Pressure Die Casting Machine, Mould or Production line, please contact us: cnkylt@aliyun.com
Related Casting Machinery:
Die Casting Machine
· Battery Spine Die Casting Machine
· Cold Chamber Die Casting Machine
· Hot Chamber Die Casting Machine
· Vertical Die Casting Machine
Material
· Aluminum Die Casting Machine
· Magnesium Die Casting Machine
Application
· Auto Parts Die Casting Machines
· Kitchen &Household Parts Die Casting Machines
· Lamps Light Parts Die Casting Machines
· Electric Vehicle Spare Parts Die Casting Machines
· Hardware, Jewelry, Clothing Accessories Die Casting Machines
· Tel-Communication Equipment Parts Die Casting Machines
· Garden Machinery & Electric Tools Parts Die Casting Machines
· Lead Acid Battery Terminal Bushing, Battery Positive Spine Grid Die Casting Machines
· Fishing Sinker Die Casting Machines
· Others
评论
发表评论