In manufacturing process, fixture is widely used. In order to save cost and use min. quantity fixtures to meet more production demand or suit for more manufacturing line use. That require fixture design to met some standard.
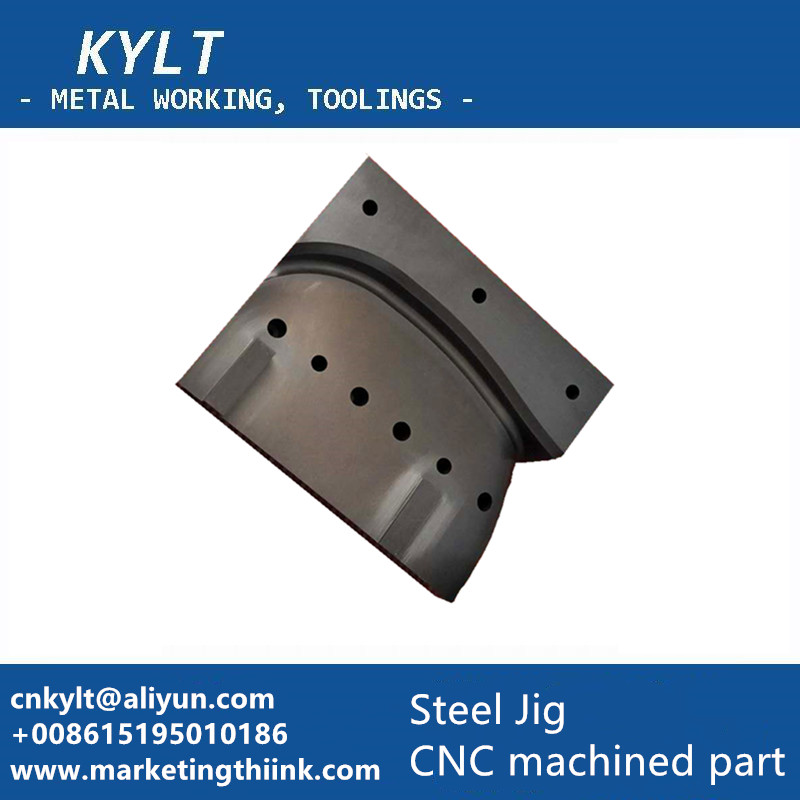
1.Basic methods and steps of fixture design
PREPARATION BEFORE DESIGN OF FIXTURE:
A) design notice, finished part drawing, blank drawing, process route and other technical data, understand the processing technical requirements of each process, positioning and clamping scheme, processing content of previous process, blank situation, machine tool, cutter, Inspection measuring tool used in processing, machining allowance and cutting amount, etc.
B) understand the production batch and the need for clamps;
C) understand the main technical parameters, performance, specification, accuracy of the machine tool used and the connection dimension of the structure of the part connected with the fixture;
D) standard stock of fixture.
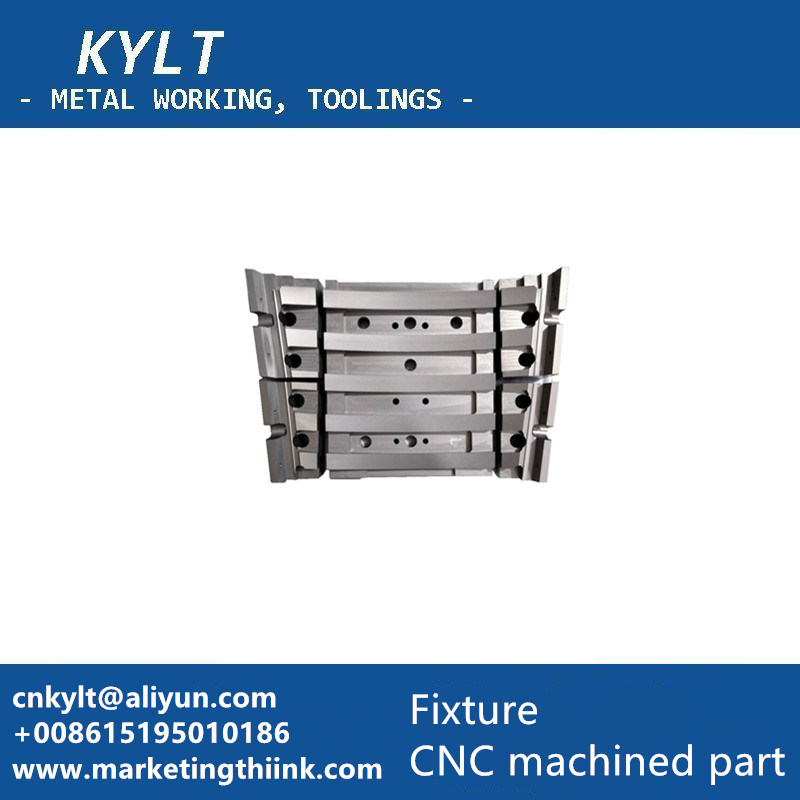
2.Problems to be considered in fixture design
Generally, the structure of fixture design is single, which gives people a feeling that the structure is not very complex. Especially now, the popularity of hydraulic fixture greatly simplifies the original mechanical structure. However, if the design process is not considered in detail, there will inevitably be unnecessary troubles:
A) BLANK ALLOWANCE OF THE WORKPIECE TO BE PROCESSED.
The size of the blank is too large, resulting in interference. So we must prepare the rough drawing before design. Leave enough space.
B) CHIP REMOVAL SMOOTHNESS OF FIXTURE.
Due to the limited machining space of the machine tool, the fixture is often designed in a compact space. At this time, it is often ignored that the iron chips generated in the machining process accumulate at the dead corner of the fixture, including the poor flow of chip liquid, which brings a lot of trouble for later processing. So at the beginning of practice, we should consider the problems in the process of machining. After all, the fixture is based on improving efficiency and convenient operation.
C) OVERALL OPENING OF FIXTURE.
Neglecting the openness makes it difficult for the operator to install the card, which is time-consuming and laborious.
D) BASIC THEORETICAL PRINCIPLES OF FIXTURE DESIGN.
Each set of fixture has to go through countless clamping and loosening actions, so it may meet the user’s requirements at the beginning, but the fixture should have its accuracy retention, so don’t design something contrary to the principle. Even if you can get away with it now, it won’t last long. A good design should be tempered by time.
E) REPLACEABILITY OF POSITIONING ELEMENTS.
The positioning element is seriously worn, so it should be considered to replace it quickly and conveniently. It is better not to design it as a large part.
The accumulation of fixture design experience is very important, sometimes design is one thing, in practical application is another thing, so good design is a process of continuous accumulation and summary.
KYLT Precision CNC machining services (milling & turning service), Fast prototyping, Fixture/Jig/Tooling making, Aluminum die casting & plastic injection parts. Email:cnkylt@aliyun.com +008615195010186
KYLT CNC Machining Services:
KYLT CNC Precision Machined Parts:
More information about Machining Technology:
评论
发表评论