Suitable for a range of metal alloys, die casting has the following advantages:
Saving cost, not only in the part price itself but also in the overall cost of production.
Produces complex parts to net shape, reducing secondary machining
High-speed production compared to other manufacturing processes
Die cast parts are durable and have a long service life
Produces components with attractive, high-quality surface finishes
Produces a broad range of shapes and surface textures
Variable wall thicknesses
Simplifies the assembly process by integrating fastening elements
Fewer steps from raw material to finished part
Tighter tolerances
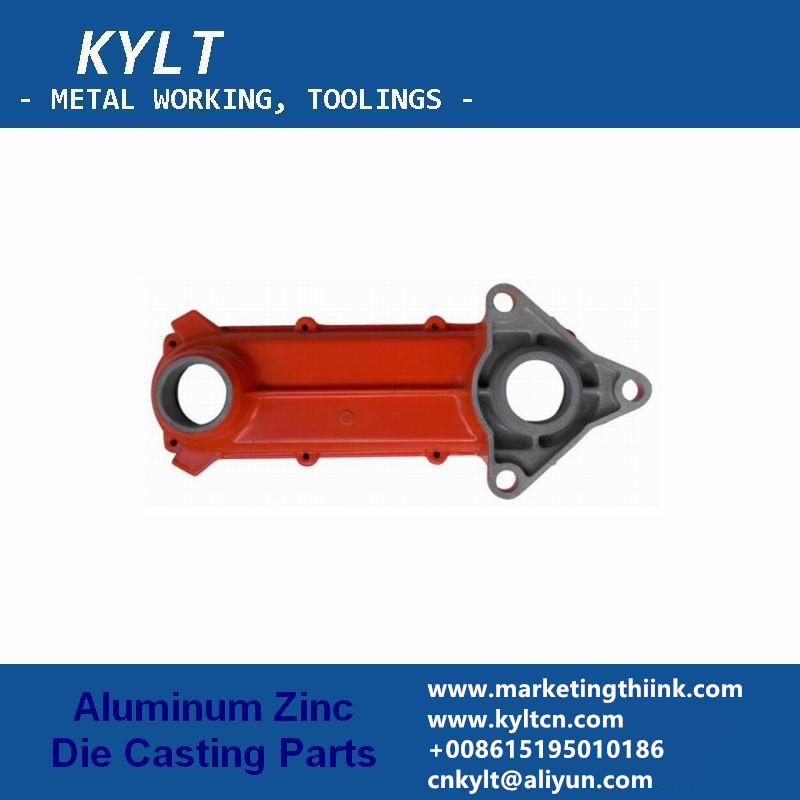
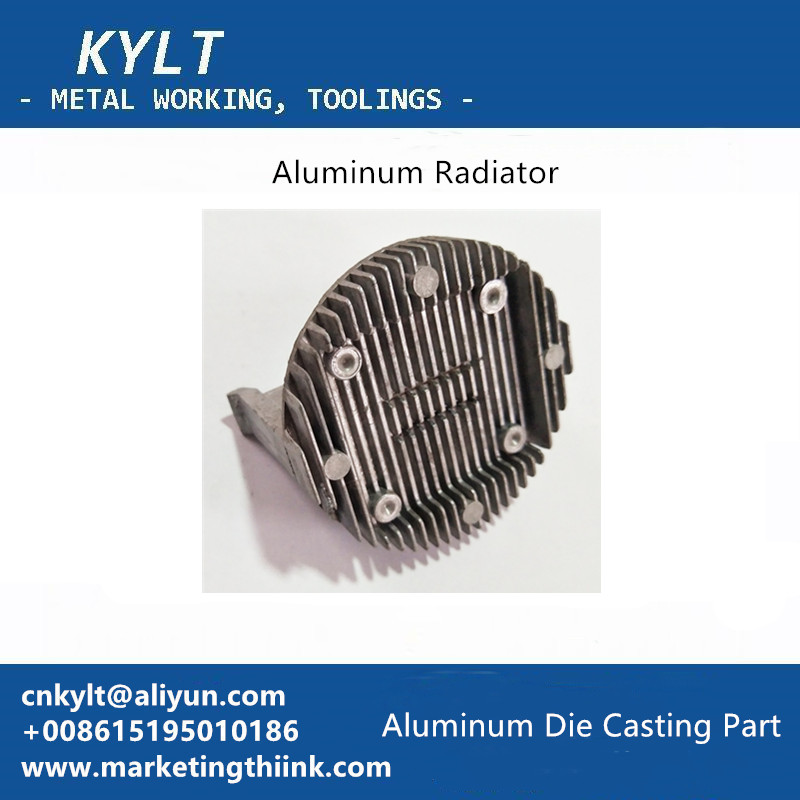
ALUMINUM DIE CASTING PARTS, MADE BY 200-500T COLD CHAMBER DIE CASTING MACHINES:
Aluminum Die Casting Part – Radiator
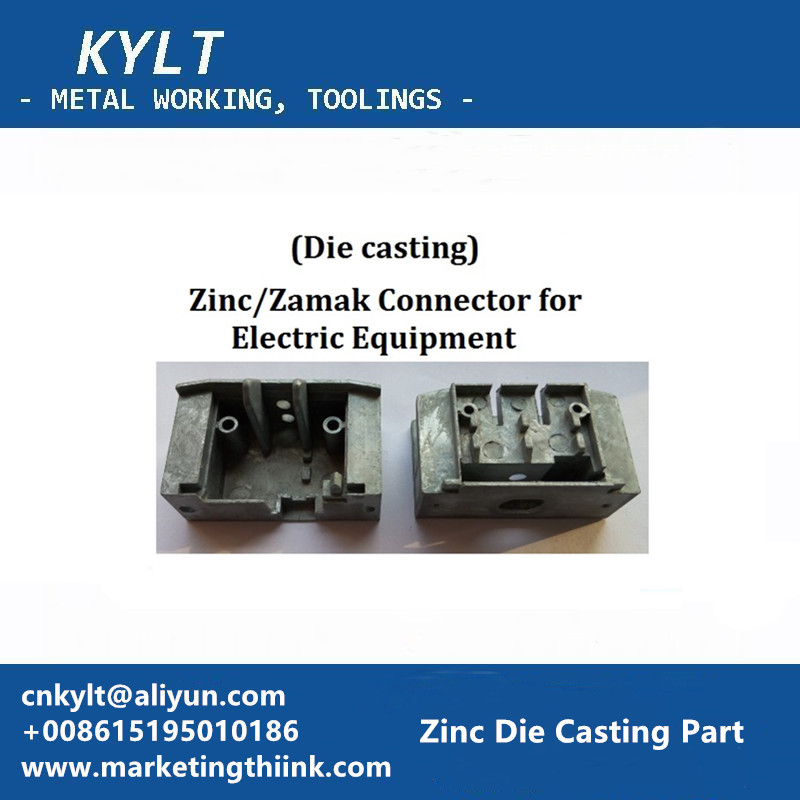
ZINC / ZAMAK DIE CASTING PARTS, SMALL SIZES PARTS MADE BY HOT CHAMBER DIE CASTING MACHINES, MIDDLE & BIG SIZES PARTS MADE BY COLD CHAMBER DIE CASTING MACHINES:
The calculation of a die casting part price involves:material cost, injection cost, trimming cost, machining cost, surface finish cost, packing cost etc.
Send your die casting project 2D/3D drawing to: cnkylt@aliyun.com , to got a free quotation now.
After the first metal part be tapped, we always to check it: if pass the thread gauge inspection? The inspection result is OK, we can do mass production. If it fails, We should consider which reasons cause tapping faiulre. KYLT provide Metal Machining services for: WEDM, EDM, DRILL, TAPPING , CNC LATHING , CNC MILLING , ALUMINUM / MAGNESIUM / PLASTIC RAPID PROTOTYPES MAKING . 1PCS ORDER IS ALLOWED. Aluminum CNC machined workpiece Normally, the following reasons may cause screw thread faiulre: 1) UNQUALIFIED TAP Tap is wear or bad 2) QUALIFIED DRILLING HOLE (BEFORE TAPPING) If the hole is too small, because of friction, will increase the difficulty of tapping, while tapping faster wear, and vice versa, the hole is too big, it can easily tap into, but the quality of teeth is very poor, because the diameter of teeth will become larger, relative to the screw nut bonding force is insufficient, easy to slide teeth. In M3 *0.5, the correct hole (general i...
When design machine parts / prototypes by 2D engineering method, we can adopt simplified drawing method: 1.When the object ( mechanical part ) has several identical structures (teeth, slots, etc.) and distributes according to certain rules, only a few complete structures need to be drawn. The rest are connected by fine lines, and the total number of structures is indicated. Mechanical part Examples of Simplified Drawing of Mechanical Drawings : Examples of Simplified Drawing of Mechanical Drawings for Same Structure and Simplified Drawing Same Structure and Simplified Drawing 2.A number of holes with the same diameter and regular distribution (round holes, screw holes, sinks, etc.) can be drawn only one or several, the rest can only be represented by the center line, and the total number of holes should be indicated when the size of holes is marked in the figure. Simplified Drawing Method for Regularly Distributed Holes Simplified Drawing ...
CNC milling process adopt Down milling or Up milling ? Which milling method is better? Down Milling & Up Milling Definition Down milling: refers to the cutting speed direction of the cutter is the same as the moving direction of the workpiece. Up milling : refers to the direction of cutting speed opposite to the direction of movement of the workpiece. CNC milling work, How to distinguish Down Milling and Up Milling. WHEN MILLING WORKPIECE OUTLINE: Clockwise feeding and programming along the outline of the workpiece is Down milling. Counterclockwise programming and feeding along the outline of the workpiece is Up milling. WHEN MILLING THE INNER CONTOUR OF THE WORKPIECE: Clockwise feeding and programming along the inner contour of the workpiece is downmilling. Counterclockwise programming and feeding along the inner contour of the workpiece is reverse milling. CNC UP & DOWN MILLING CHARACTERISTICS OF DOWN MILLING AND UP MILLI...


评论
发表评论