跳至主要内容

CLEAN BURRS BY ELECTROLYTIC METHOD

Electrolytic burrs cleaning method is suitable for non-ferrous and ferrous metal parts. Especially for parts with complex shapes, inner holes, cross holes and inner surface burrs that are difficult to remove by mechanical and manual methods. And can remove the burrs of extremely hard parts such as molybdenum, nickel, titanium and quenched parts.
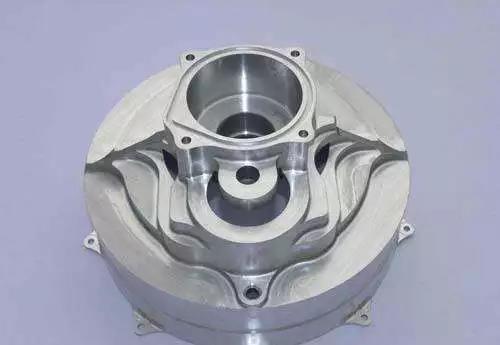
Working principle of Electrolytic burrs cleaning method

This is to use electric and chemical energy to dissolve the anode and remove the burr. The positive side of the part and the DC power supply is the anode, and the negative side of the forming tool and the DC power supply is the cathode. There is a certain gap between the two sides to let the electrolyte circulate.
When the anode and the cathode are immersed in the solution and connected to the direct current, the electrochemical reaction occurs on the anode surface, the metal dissolved on the part surface forms viscous liquid with the electrolyte, which is concentrated in the low concave part of the part surface, with high resistance and small corrosion. While the burr protrudes from the part surface, under the influence of the temperature difference, the liquid film is difficult to form, and the power line is highly concentrated in the burr part after the power is connected The burr closest to the cathode will be dissolved at the fastest speed until all the burr is dissolved and the edge will gradually form a fillet, that is to achieve the purpose of deburring.
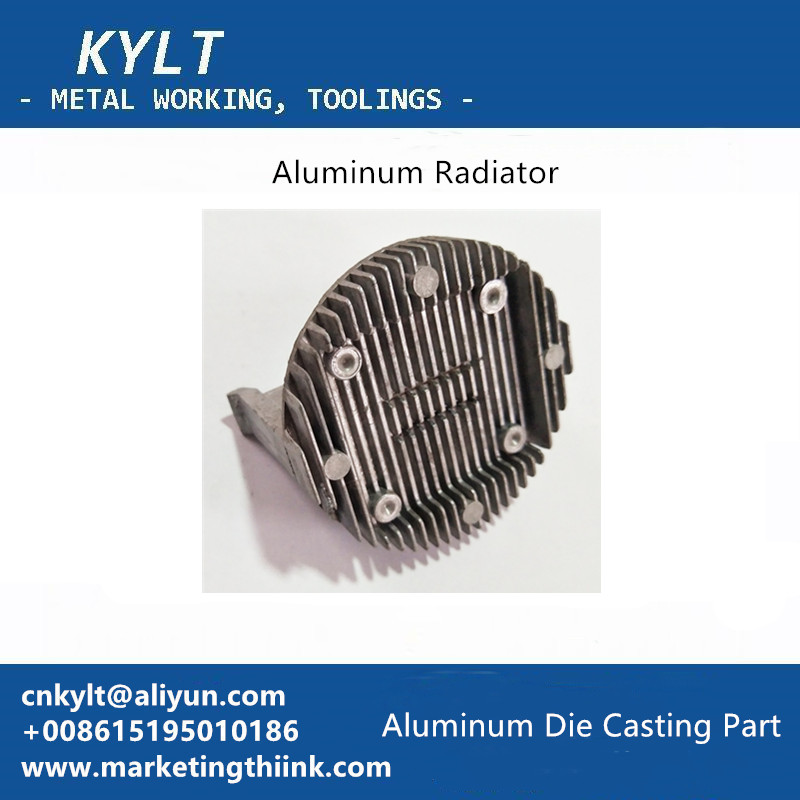
Aluminum Die Casting Radiator

Electrolytic deburring machine can be used.

When the production batch is not large, the rectifier AC can be changed into DC to make simple equipment. According to the structure of the parts, special clamps (tool cathodes) similar to the shape of the parts are made of brass or copper and other conductive materials, and the unprocessed parts are coated with epoxy resin for isolation protection. The common electrolytes are NaCl, NaNO2 and NaNO3 solutions.
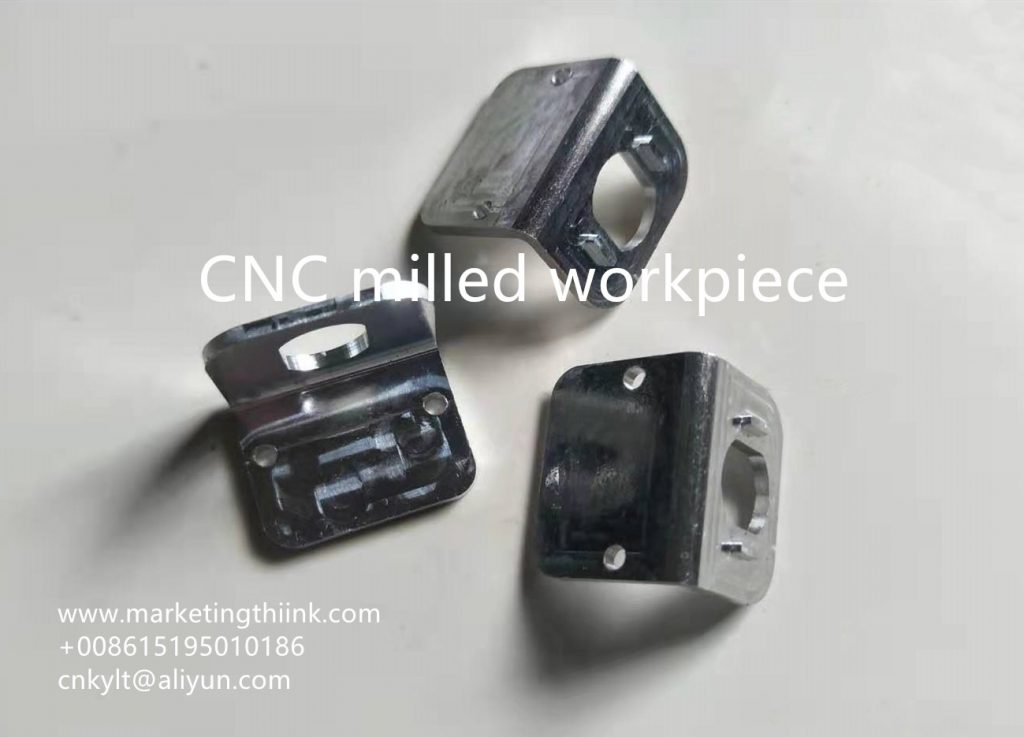
CNC milled workpiece
KYLT Precision CNC machining services (milling & turning service), Fast prototyping, Fixture/Jig/Tooling making,Aluminum die casting & plastic injection parts. Email:cnkylt@aliyun.com +008615195010186
KYLT CNC Machining Services:
KYLT CNC Precision Machined Parts:
More information about Machining Technology:

评论

此博客中的热门博文

SIMPLIFIED DRAWING METHOD FOR MECHANICAL DRAWING

When design  machine parts  /  prototypes  by 2D engineering method, we can adopt simplified drawing method: 1.When the object ( mechanical part ) has several identical structures (teeth, slots, etc.) and distributes according to certain rules, only a few complete structures need to be drawn. The rest are connected by fine lines, and the total number of structures is indicated. Mechanical part  Examples of Simplified Drawing of Mechanical Drawings : Examples of Simplified Drawing of Mechanical Drawings for Same Structure and Simplified Drawing Same Structure and Simplified Drawing 2.A number of holes with the same diameter and regular distribution (round holes, screw holes, sinks, etc.) can be drawn only one or several, the rest can only be represented by the center line, and the total number of holes should be indicated when the size of holes is marked in the figure. Simplified Drawing Method for Regularly Distributed Holes Simplified Drawing ...

WHY SCREW THREAD CAN NOT PASS THREAD GAUGE INSPECTION

After the first metal part be tapped, we always to check it: if pass the thread gauge inspection? The inspection result is OK, we can do mass production. If it fails, We should consider which reasons cause tapping faiulre. KYLT provide Metal Machining services for:  WEDM, EDM, DRILL, TAPPING ,  CNC LATHING ,  CNC MILLING ,  ALUMINUM / MAGNESIUM / PLASTIC RAPID PROTOTYPES MAKING . 1PCS ORDER IS ALLOWED. Aluminum CNC machined workpiece Normally, the following reasons may cause screw thread faiulre: 1) UNQUALIFIED TAP Tap is wear or bad 2) QUALIFIED DRILLING HOLE (BEFORE TAPPING) If the hole is too small, because of friction, will increase the difficulty of tapping, while tapping faster wear, and vice versa, the hole is too big, it can easily tap into, but the quality of teeth is very poor, because the diameter of teeth will become larger, relative to the screw nut bonding force is insufficient, easy to slide teeth. In M3 *0.5, the correct hole (general i...

CNC MILLING: DOWN MILLING &UP MILLING

CNC milling  process adopt  Down milling  or  Up milling ? Which milling method is better? Down Milling & Up Milling Definition Down milling:  refers to the cutting speed direction of the cutter is the same as the moving direction of the workpiece. Up milling : refers to the direction of cutting speed opposite to the direction of movement of the workpiece. CNC milling work, How to distinguish Down Milling and Up Milling. WHEN MILLING WORKPIECE OUTLINE: Clockwise feeding and programming along the outline of the workpiece is Down milling. Counterclockwise programming and feeding along the outline of the workpiece is Up milling. WHEN MILLING THE INNER CONTOUR OF THE WORKPIECE: Clockwise feeding and programming along the inner contour of the workpiece is downmilling. Counterclockwise programming and feeding along the inner contour of the workpiece is reverse milling. CNC UP & DOWN MILLING CHARACTERISTICS OF DOWN MILLING AND UP MILLI...